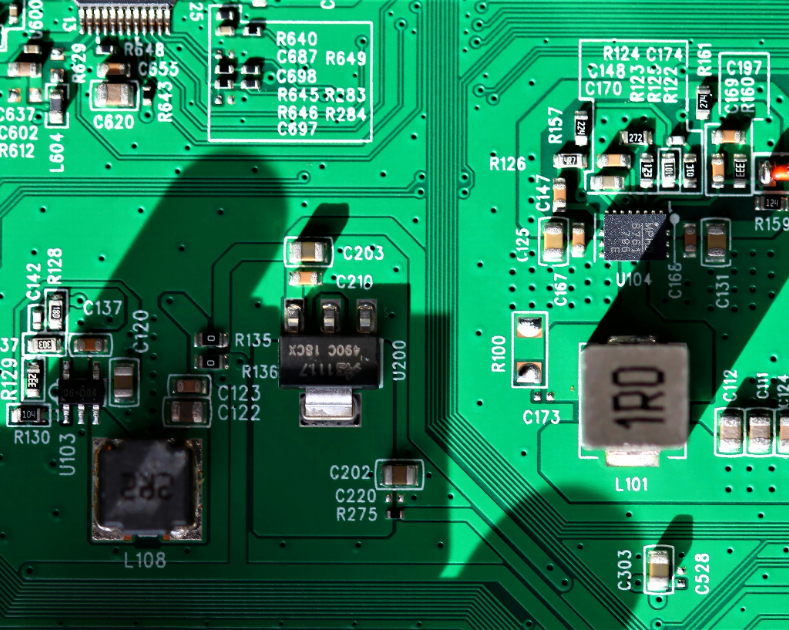
PCB assembly failures can cause field returns, delayed shipments, and costly rework. A reliable root cause analysis process connects PCB inspection, solder joint defects, and SMT assembly data to the actual process step. The goal is not only to repair one failed board, but also to stop the same failure from returning. This guide explains the most common defects, the evidence to collect, and the corrective actions that give the fastest results. It is written for overseas buyers, distributors, engineers, and purchasing teams working with a PCB assembly supplier.
1. What Counts as a PCB Assembly Failure?
A PCB assembly failure occurs when a finished board does not meet its electrical, mechanical, visual, or reliability requirements. The board may fail during production testing, final inspection, system integration, environmental testing, or use in the field. Some failures are easy to see, such as a missing component. Others need electrical testing, AOI, X-ray inspection, or microscopic analysis.
A single failed board does not always prove a process problem. However, repeated failures usually point to a broken control in the design, material, machine, method, measurement, or work environment. This is why a repair action alone is not enough. A good supplier must find the physical failure mode and then verify the process cause.
| Failure stage | Typical symptom | Best first check |
|---|---|---|
| Incoming material | Wrong part, damaged package, poor solderability | Part number, date code, moisture and packaging records |
| SMT placement | Missing, shifted, reversed, or wrong component | Placement file, feeder setup, AOI images, machine logs |
| Reflow soldering | Open joint, bridge, void, tombstone, poor wetting | Thermal profile, paste condition, pad design, X-ray results |
| Through-hole soldering | Insufficient fill, solder bridge, lifted lead | Lead cut, hole size, solder wave or selective solder settings |
| Testing | Intermittent signal, short circuit, no power | Test fixture, net list, schematic, power rail measurement |
| Field use | Early life failure, heat damage, intermittent operation | Failure history, operating conditions, cross-section and stress test |
2. The Most Common PCB Assembly Failures
2.1 Solder bridges and short circuits
A solder bridge is an unwanted connection between two pads, pins, or copper features. It is common on fine-pitch integrated circuits, connectors, and small passive components. A bridge may be visible under magnification, but a hidden short under a package may require X-ray inspection or electrical test.
Common causes include too much solder paste, damaged stencil apertures, poor board support, incorrect component placement, excessive paste offset, and an unsuitable reflow profile. Pad spacing and solder mask design can also make bridging more likely.
Root cause evidence: Compare the solder paste inspection result with the AOI image. If paste volume is high before placement, check the stencil and printer. If paste is correct but the solder spreads during reflow, check the thermal profile, pad design, and board cleanliness.
2.2 Solder opens and poor wetting
An open solder joint does not create a reliable electrical or mechanical connection. It may look like a dull joint, a joint with incomplete wetting, or a pin that appears connected but fails during continuity testing. Opens are frequent on large ground pads, connector pins, thermal pads, and areas with poor solder paste transfer.
Possible causes include low paste volume, blocked stencil apertures, oxidation, insufficient heat, a contaminated pad, component warpage, and an incorrect land pattern. Lead-free solder also needs a controlled thermal profile because insufficient heat can prevent proper wetting.
Root cause evidence: Check paste volume, solderability records, reflow temperature, and the failure location. If all open joints occur on one component type, investigate its package, pad layout, or supply batch. If they occur across the whole panel, investigate printing, paste storage, or reflow conditions.
2.3 Tombstoning and component standing
Tombstoning happens when one end of a small two-terminal component lifts from the PCB during reflow. The component stands at an angle like a small tombstone. It creates an open circuit and may also damage the pad or nearby component.
The main cause is an uneven force on the two terminals. Uneven solder paste volume, different pad thermal mass, unequal copper areas, placement offset, and uneven heating can create this force. Tombstoning is more common with small passive parts such as 0201, 0402, and 0603 packages.
Corrective action: Balance the pad design, control paste deposition, check component centering, and review the heating rate. A controlled preheat zone can reduce uneven thermal stress. Do not solve every tombstone by simply adding more solder paste.
2.4 Component misalignment and placement shift
A component may be rotated, shifted, tilted, or placed on the wrong pads. Small placement errors can produce an open circuit, a short circuit, poor mechanical clearance, or a failure during connector assembly. The defect may come from the PCB design or from the assembly process.
Typical causes include an incorrect centroid file, wrong feeder setup, poor fiducial recognition, board movement, worn machine nozzles, inaccurate library data, and excessive solder paste movement during reflow. A component can also move if the paste is too wet or the board is not supported correctly.
| Placement defect | Likely cause | Useful verification |
|---|---|---|
| Wrong component | Feeder or bill of materials error | Scan part label and compare with the approved BOM |
| Wrong rotation | Library or centroid orientation error | Compare CAD data, machine program, and first article image |
| Shifted component | Fiducial, nozzle, paste, or board support issue | Review placement coordinates and AOI position data |
| Missing component | Pick failure, empty feeder, or programming error | Check feeder alarms, material count, and AOI records |
2.5 Insufficient solder and excessive solder
Too little solder reduces joint strength and may create an open connection. Too much solder can cause bridges, poor component seating, and hidden voids. Both defects can result from the same control problem: unstable solder paste printing.
Important variables include stencil thickness, aperture size, paste age, paste temperature, squeegee pressure, print speed, separation speed, board support, and cleaning frequency. A printer can produce acceptable boards at the start of a run and poor boards later if paste dries on the stencil.
Practical check: Measure paste volume at the start, middle, and end of the production run. A single measurement cannot show process drift. Use solder paste inspection data to identify whether the problem is on one pad, one component group, one board edge, or the whole panel.
2.6 Voids in solder joints
A void is a gas-filled space inside a solder joint. Small voids may be acceptable under the customer specification, but large or repeated voids can reduce thermal transfer and mechanical strength. Voids are especially important under power devices, LED packages, and exposed-pad components.
Voids are not normally confirmed by visual inspection. X-ray inspection is the usual method. Possible causes include trapped flux gas, excessive paste volume, poor stencil aperture design, fast heating, unsuitable soak conditions, and contamination.
The correct response depends on the joint function. A void under a small signal resistor may have a different risk from a void under a power transistor. The supplier should record void size, position, and percentage instead of using the simple description of bad solder.
2.7 Delamination, pad lifting, and PCB damage
PCB damage may appear as lifted pads, burned laminate, blistering, cracked vias, or delamination between board layers. It can happen during rework, depanelization, connector insertion, screw installation, or thermal cycling.
Common causes include excessive rework temperature, repeated heating, poor laminate quality, incorrect drill settings, sharp depanelization stress, and mechanical force during assembly. Moisture absorbed by the PCB can also expand during heating and damage the board structure.
Root cause evidence: Check the board material certificate, baking records, rework temperature, number of repair cycles, routing method, and cross-section results. A lifted pad found after manual rework may be a handling failure rather than a reflow failure.
2.8 Wrong, missing, or damaged components
A wrong component can pass visual inspection when two parts have similar packages. The electrical value, tolerance, voltage rating, firmware version, or polarity may still be incorrect. Missing components and damaged parts create similar production and field symptoms.
Strong material control starts with an approved bill of materials, supplier part numbers, manufacturer part numbers, and revision control. Barcode scanning, feeder verification, first article inspection, and automatic optical inspection add more protection.
Component damage may result from electrostatic discharge, moisture, excessive heat, mechanical impact, or incorrect storage. Moisture-sensitive devices should remain in controlled packaging and should be tracked with floor life records after opening.
2.9 Polarity and orientation errors
Diodes, electrolytic capacitors, LEDs, connectors, integrated circuits, and power modules may fail if they are installed in the wrong direction. The board may show no power, excessive current, heat damage, or an unsafe operating condition.
Polarity errors often come from unclear silkscreen marks, incorrect library data, inconsistent component drawings, or a mismatch between the BOM and placement file. The design should show a clear pin one mark and a clear positive or negative mark where needed.
Prevention method: Confirm polarity at three points: engineering data review, first article inspection, and AOI programming. Do not rely on one visual mark or on operator memory.
2.10 Cold solder joints and non-wetting
A cold solder joint may have a rough appearance, incomplete bonding, or weak mechanical strength. Non-wetting occurs when solder does not properly spread across the pad and component termination. The joint may work during a basic test and fail later under vibration or thermal cycling.
Possible causes include oxidation, contamination, low temperature, short contact time, unsuitable surface finish, expired paste, and incorrect reflow settings. A large copper area may also remove heat faster than expected.
The best investigation compares good and bad joints by using microscope images, solderability information, and the actual thermal profile. Changing the reflow recipe without checking material condition can hide the problem instead of correcting it.
3. Root Cause Analysis: The Difference Between Symptom and Cause
The symptom is what the inspector or customer sees. The failure mode describes how the board failed. The root cause explains why the process allowed the failure to happen. These three terms should not be mixed.
| Level | Example |
|---|---|
| Symptom | Board does not start |
| Failure mode | Short circuit between two power nets |
| Physical cause | Solder bridge under a fine-pitch IC |
| Process cause | Stencil aperture released excessive paste |
| System cause | New stencil was used without an approved design review |
A repair technician may remove the bridge and make the board work. That action fixes the symptom on one unit. It does not prove that the next board will be safe. Root cause analysis must continue until the cause can be tested and the corrective action prevents recurrence.
4. A Step-by-Step PCB Failure Investigation Process
Use the following process for customer returns, production defects, intermittent failures, and repeated quality issues. Keep the steps in order. Skipping evidence collection often leads to a quick but incorrect conclusion.
- Contain the problem.
- Define the failure mode.
- Collect traceable evidence.
- Separate good boards from failed boards.
- Inspect without changing the evidence.
- Test the electrical and mechanical behavior.
- Trace the failure back to the process.
- Confirm the root cause with a controlled test.
- Apply corrective and preventive action.
- Verify the result with later production data.
Step 1: Contain the problem
Stop shipment when the failure could affect other units. Identify the affected lot, date, shift, machine, operator, material batch, and PCB panel. Quarantine finished boards, work in progress, and remaining components when they share the same risk.
Containment should be specific. For example, hold boards made on Line 2 between 08:00 and 12:00, rather than placing every customer order on hold without evidence. Record the containment decision and the person who approved it.
Step 2: Define the failure mode
Write the failure in measurable terms. "Bad solder" is too general. A better statement is "Three of 40 boards show an open connection on pin 12 of U3 after reflow and functional test." Include the test method, limit, location, and failure rate.
Separate failure modes if they have different evidence. A solder bridge, a missing component, and an incorrect firmware version should not be placed in one general defect category. Clear definitions make trends easier to see.
Step 3: Collect traceable evidence
Collect the customer failure report, photos, failed units, good units, BOM revision, Gerber files, pick-and-place files, stencil drawing, reflow profile, solder paste lot, component lot, AOI records, SPI records, test results, and operator notes.
Traceability should connect the board serial number to the PCB lot, assembly date, machine line, material batches, inspection records, and repair history. Without this connection, the investigation becomes an opinion based on a small sample.
Step 4: Inspect before repair
Photograph the failed unit before cleaning, rework, or component removal. Use visual inspection, microscope inspection, AOI review, X-ray inspection, and electrical testing as appropriate. Mark the exact failure location on a board drawing.
Do not scrape solder or replace a component before recording the original condition. Rework can remove important evidence, such as paste spread, pad damage, component cracking, or the direction of a lifted lead.
Step 5: Compare failed and good samples
A good comparison uses several failed boards and several passing boards from the same lot. Compare component position, solder shape, pad condition, X-ray images, test values, thermal history, and material history.
If every failed board has the same location and the same physical condition, the cause may be localized. If failures are random across the panel, investigate process variation, handling, or test fixture reliability.
Step 6: Use the right inspection method
| Inspection method | Finds | Limit |
|---|---|---|
| Visual inspection | Missing parts, obvious bridges, damage, polarity marks | Cannot see hidden joints or many small defects |
| Microscope inspection | Fine-pitch solder shape, cracks, pad damage | Needs access and cannot confirm all electrical faults |
| SPI | Solder paste height, area, volume, offset | Checks paste before reflow, not the final joint |
| AOI | Placement, polarity, bridges, open-looking joints | May miss hidden joints and some false calls need review |
| X-ray inspection | Hidden solder joints, voids, BGA defects, underside bridges | Requires correct image interpretation |
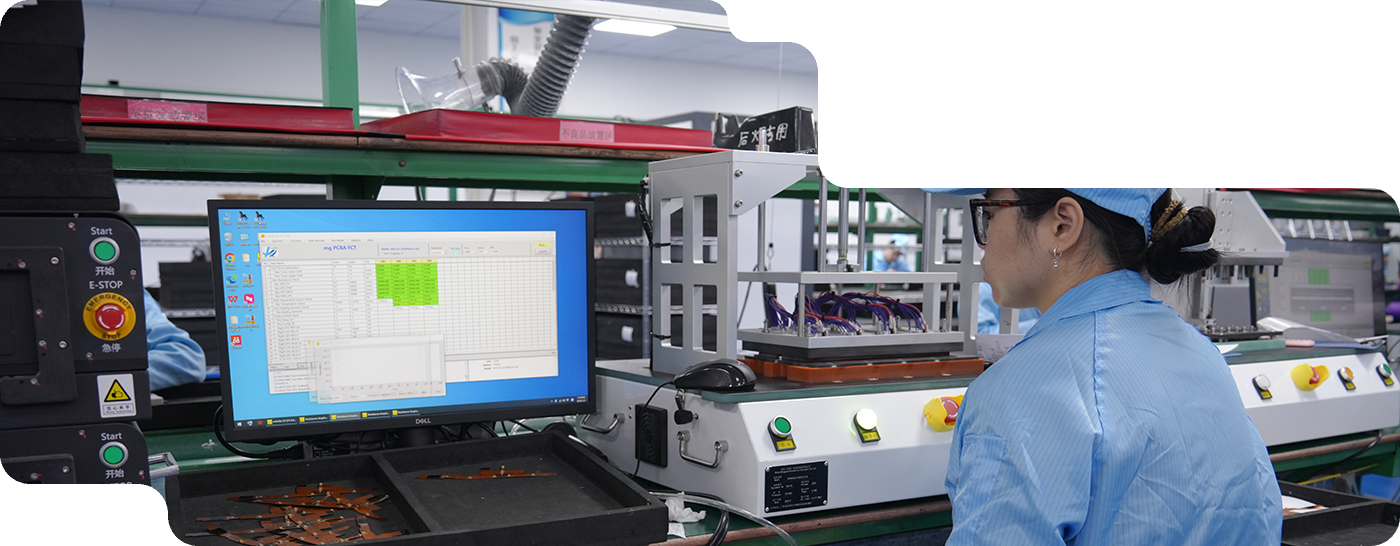
| ICT or flying probe | Opens, shorts, values, some component faults | Test access and fixture quality affect results |
| Functional test | System operation under defined conditions | May not identify the exact physical defect |
| Cross-section | Internal layers, barrels, solder interfaces | Destructive and should be used on selected samples |
Step 7: Build a cause and effect chain
Use the 5 Whys method, a fishbone diagram, or a process map. Review six cause groups: material, machine, method, measurement, manpower, and environment. Ask for evidence at every level.
Example: The board failed the power test. Why? A capacitor was shorted. Why? It was installed in the wrong position. Why? The feeder label did not match the machine program. Why? The program revision was released without a second-person verification. The system cause is weak revision control, not only operator error.
Step 8: Confirm the suspected cause
A suspected cause becomes stronger when a controlled test reproduces the defect or when a controlled change removes it. For example, compare the original stencil aperture with a corrected aperture on a limited trial panel. Measure paste volume, inspect the joints, and run electrical tests.
Do not change several variables at once unless safety requires it. If the stencil, paste, reflow profile, and placement program all change together, the team may not know which change solved the problem.
Step 9: Apply corrective and preventive action
Corrective action removes the current cause. Preventive action improves the system so that the same type of failure is less likely on future products. Examples include changing a stencil aperture, updating the approved BOM, adding a feeder scan, improving board support, revising work instructions, or adding a test point.
Step 10: Verify effectiveness
Define the verification period before closing the issue. It may be the next three production lots, the next 1,000 boards, or a defined environmental test. Record the defect rate before and after the action. A process is not proven stable because one repaired board passed.
5. How to Use Data Instead of Guesswork
Quality teams should calculate the defect rate by lot, line, component, defect type, and process step. Useful measurements include defects per million opportunities, defects per board, first pass yield, rework rate, escape rate, and customer return rate.
For a simple defect rate, divide the number of defective boards by the number of inspected boards and multiply by 100. If 18 boards fail out of 1,200 inspected boards, the board defect rate is 1.5 percent. If one board has four defects, also report the defect count because board rate and defect rate are different measures.
| Data pattern | Likely direction of investigation |
|---|---|
| Defects increase after a new stencil is installed | Stencil design, thickness, aperture release, approval control |
| Defects appear on one panel edge | Board support, warpage, print pressure, thermal balance |
| Defects increase late in the shift | Paste drying, temperature, cleaning interval, operator workload |
| Only one component lot fails | Package dimensions, solderability, moisture, supplier quality |
| Failures occur only during system test | Power sequence, firmware, fixture, connector, functional load |
| Failures appear after thermal cycling | Joint fatigue, PCB warpage, component cracking, material mismatch |
Trend charts are more useful than one final inspection number. A rising defect rate can show process drift before the customer receives a failure. For overseas buyers, a supplier should be able to provide lot records, inspection summaries, and a clear 8D or corrective action report when the issue is serious.
6. Failure Analysis by PCB Assembly Process Step
6.1 Design and DFM review
Some assembly failures begin before the first board is built. A pad that is too small, an incorrect pin one mark, poor component spacing, an inaccessible test point, or an unbalanced copper area can create repeated production problems.
A design for manufacturing review should check component spacing, solder mask clearance, fiducials, panel rails, thermal relief, stencil access, package direction, alternate parts, board thickness, and test coverage. The review should use the final manufacturing files, not an old drawing.
6.2 Incoming inspection
Incoming inspection confirms that the PCB, components, solder paste, and other materials match the purchase and engineering requirements. Check quantity, part number, package, date code, moisture label, damage, surface finish, and certificate information.
Do not assume that a sealed bag guarantees a correct part. A wrong label, mixed reel, counterfeit component, or damaged package can create a failure that looks like an assembly problem.
6.3 Solder paste printing
Printing is one of the most important control points in SMT assembly. Stable printing depends on paste condition, stencil condition, board support, alignment, pressure, speed, and cleaning. SPI gives early evidence before the component is soldered.
When the defect is a bridge or open, compare the SPI volume and offset for the exact pads. This often separates a printing cause from a placement or reflow cause in less time.
6.4 Pick and place
Check feeder setup, nozzle condition, component recognition, fiducial accuracy, placement force, and machine alarms. A placement machine can run at normal speed while producing a repeated wrong rotation if the library data is incorrect.
First article approval is important after a new program, new board revision, new component, or machine change. The approved sample should show reference designators, component values, orientation, and critical dimensions.
6.5 Reflow soldering
The reflow profile must match the solder paste and the board assembly. Measure the profile on representative locations, including large copper areas and heat-sensitive components. A profile measured once on an empty carrier may not represent the production condition.
Review ramp rate, soak time, peak temperature, time above liquidus, cooling rate, conveyor speed, and actual board temperature. Keep the profile record with the product lot and paste lot.
6.6 Through-hole and selective soldering
Through-hole failures include insufficient barrel fill, solder bridges, pin shorts, lifted leads, and poor wetting. Causes may include incorrect lead length, blocked holes, poor flux application, wrong preheat, wave shadowing, or poor fixture design.
For selective soldering, confirm nozzle position, solder temperature, dwell time, flux volume, and board orientation. Large connectors and thermal terminals often need separate process settings.
6.7 Cleaning, coating, and final assembly
Residue left on the board may cause leakage current, corrosion, or intermittent operation. Excess cleaning pressure can damage components or move small parts. Conformal coating can fail because of contamination, bubbles, poor masking, or incorrect curing.
Final assembly adds mechanical risks. Over-tightened screws, connector force, cable strain, heat sinks, and enclosure pressure can crack solder joints or warp the PCB. A failure found after final assembly may not be caused by SMT placement.
7. Common Root Cause Tools and When to Use Them
| Tool | Best use | Key question |
|---|---|---|
| 5 Whys | Simple repeated failure with a clear process path | Why did the control allow this defect? |
| Fishbone diagram | Complex or cross-functional problems | Which cause group has supporting evidence? |
| Pareto chart | Many defect types compete for attention | Which small number of causes creates most defects? |
| Process flow chart | Failures may occur at several stages | Where was the defect created or missed? |
| Gage R and R study | Test or measurement disagreement | Can the inspection system measure the defect reliably? |
| Design of experiments | Several process variables may interact | Which variables have the strongest effect? |
| 8D report | Customer complaint and formal corrective action | How was the issue contained, corrected, and prevented? |
Measurement system analysis should not be overlooked. If two inspectors disagree about a solder joint, the team may be investigating an inspection method instead of a production failure. Define the acceptance standard, use approved samples, and confirm that AOI, X-ray, ICT, and functional test equipment are calibrated.
8. PCB Assembly Failure Investigation Flow Chart
Customer or production failure reported | v Contain affected boards and preserve samples | v Define symptom, location, test condition, and failure rate | v Inspect failed units before repair | v Is there a visible or measurable physical defect? | +----+----+ | | Yes No | | v v Classify Confirm test method, fixture, failure power, software, and environment | | v v Check SPI, AOI, X-ray, test, material, and process records | v Compare failed units with passing units | v Form a cause and effect chain | v Run a controlled confirmation trial | v Apply corrective action and preventive action | v Verify the next defined lot or test sample | v Close the report only when evidence shows controlThis flow is useful because it prevents teams from starting with a favorite explanation. It also creates a clear record for the customer. A report should show what was observed, what was tested, what was changed, and how the change was verified.
9. Example: Finding the Root Cause of a Repeated BGA Failure
Suppose a customer reports that a control board fails during system start-up. The first visual inspection shows no defect. Electrical testing identifies an open connection under a BGA device. X-ray inspection finds that the open occurs on several balls near one board edge.
The team compares ten failed boards with ten passing boards. The failed boards show lower solder volume on the same BGA area. SPI data shows a paste offset toward the panel edge. The board support pins are missing under that area, allowing slight board movement during printing.
A controlled trial adds support pins and improves the stencil opening for the affected pads. The next trial lot shows stable paste volume, and all sample boards pass electrical testing. The root cause is not simply "BGA open." The stronger conclusion is that inadequate board support caused paste offset and low solder volume in a repeated location.
| Investigation item | Finding | Decision |
|---|---|---|
| Customer symptom | Start-up failure | Run electrical and functional confirmation |
| Failure mode | Open BGA connection | Use X-ray and selected cross-section |
| Pattern | Same board edge and same device area | Check panel support and thermal balance |
| SPI result | Low paste volume and offset | Investigate printing, not only reflow |
| Process cause | Insufficient support under the BGA area | Change support tooling and validate |
10. How to Prevent PCB Assembly Failures Before Production
Use controlled engineering data
Keep the BOM, Gerber files, pick-and-place file, schematic, assembly drawing, test program, and work instructions under revision control. Every change should have an owner, approval date, and clear effect on production.
Approve the first article
Build a first article after a new product introduction, major design change, new supplier, or process change. Confirm every reference designator, value, package, polarity, orientation, and critical solder joint before volume production.
Control moisture-sensitive materials
Track moisture-sensitive components, floor life, bake conditions, storage temperature, and humidity. Keep opened materials in the required dry environment. Record the time out of controlled packaging.
Maintain machines and tooling
Clean printers, inspect stencils, replace worn nozzles, calibrate placement machines, verify feeders, and maintain reflow ovens. A preventive maintenance schedule should include actual checks, limits, results, and responsible personnel.
Use layered inspection
No single inspection method finds every defect. SPI checks paste, AOI checks many visible assembly conditions, X-ray checks hidden joints, and electrical tests check circuit behavior. Use a combination based on product risk and customer requirements.
Design for test and repair
Add test points for critical nets, provide safe probe access, separate high-risk power sections, and leave enough space for inspection and rework. Test coverage reduces the chance that an assembly defect reaches the customer.
11. What Overseas Buyers Should Ask a PCB Assembly Supplier
- What inspection methods are used before and after reflow?
- Can the supplier provide SPI, AOI, X-ray, ICT, or functional test records?
- How are BOM revisions and component substitutions controlled?
- How are moisture-sensitive components stored and tracked?
- How is the reflow profile measured and connected to the production lot?
- What is the process for customer complaints and 8D reports?
- How are failed boards preserved before repair?
- What traceability is available for materials, operators, machines, and dates?
- How is corrective action verified after implementation?
- Can the supplier support DFM review before mass production?
A capable one stop pcb assembly partner should answer these questions with records, not only general promises. Buyers should also request a sample quality report, acceptance criteria, test coverage statement, and escalation contact before placing a large order.
12. How Benewave Supports PCB Assembly Failure Prevention
Benewave can support overseas customers through the complete PCB assembly process, from engineering review and component sourcing to SMT placement, soldering, inspection, testing, and shipment. The purpose of one stop service is to reduce handoff errors between separate suppliers and keep the product history in one controlled process.
For a new project, the investigation should start before production. Benewave can review the BOM, PCB files, component availability, package risks, polarity marks, test needs, and manufacturing limits. This early review can identify risks that would otherwise appear as repeated solder defects or assembly delays.
For a field or production failure, provide the board serial number, failure description, operating condition, photos, test data, and return samples when possible. Clear evidence helps the supplier separate a PCB manufacturing defect from a system, software, installation, or environmental problem.
Quality work does not end when a board passes final inspection. The supplier should track corrective action, monitor later lots, and communicate the result in a simple report. This gives distributors and overseas buyers a stronger basis for customer support and product planning.
13. Quick Root Cause Checklist
| Question | Yes or no record |
|---|---|
| Were all affected lots and boards contained? | Record lot numbers and quantity |
| Was the failure defined with a measurable test result? | Record limit and actual value |
| Were failed boards photographed before repair? | Keep images with serial numbers |
| Were good and failed boards compared? | Record sample size and pattern |
| Were SPI, AOI, X-ray, and electrical results reviewed? | Use the methods that fit the defect |
| Were material, machine, method, measurement, people, and environment checked? | List evidence for each group |
| Was the suspected cause confirmed by a controlled change? | Record trial conditions and results |
| Was a preventive action added to the process? | Update documents, training, or controls |
| Was effectiveness checked on later production? | Define lots, quantity, and acceptance target |
14. Final Answer: The Fastest Way to Find the Real Cause
The fastest reliable method is to contain the affected lot, define the exact failure mode, preserve the failed board, compare it with passing boards, and review evidence from each process step. Use SPI for solder paste, AOI for visible assembly defects, X-ray for hidden joints, and electrical testing for opens and shorts. Then use a cause and effect chain to connect the physical defect to the process control that failed.
Do not close an issue after repairing one board. Confirm the suspected cause with a controlled trial, apply corrective and preventive action, and verify the next production lots with measured data. This approach turns common PCB assembly failures into controlled manufacturing problems and helps reduce rework, customer complaints, and field returns.
When selecting a PCB assembly supplier, look for clear traceability, controlled engineering data, reliable inspection, responsive failure analysis, and documented corrective action. A supplier such as Benewave can help buyers manage the complete process from design review to final testing, while keeping quality information connected throughout production.
Frequently Asked Questions About PCB Assembly Failures
What is the most common cause of PCB assembly failure?
There is no single cause for every product. Common causes include solder paste printing variation, wrong or missing components, placement errors, poor reflow control, PCB design problems, material damage, and test fixture errors. The failure pattern and inspection evidence should determine the investigation direction.
How do you find the root cause of a solder joint failure?
First define whether the joint is open, bridged, cracked, poorly wetted, or voided. Then compare failed and passing joints, review paste data, check the reflow profile, confirm pad and component condition, and use X-ray or cross-section when needed. A controlled process change should confirm the cause.
Can AOI find all PCB assembly defects?
No. AOI is useful for many visible defects, including missing parts, wrong placement, polarity errors, bridges, and some open-looking joints. It cannot reliably inspect every hidden connection, internal BGA joint, or electrical behavior. X-ray, ICT, flying probe, and functional testing may be needed.
Why do PCB solder bridges happen?
Solder bridges can result from excessive paste, poor stencil apertures, paste offset, pad design, board movement, component placement error, or unsuitable reflow conditions. SPI data helps show whether the bridge started with too much or misplaced solder paste.
How can PCB assembly defects be reduced?
Use a DFM review, approved engineering data, controlled materials, stable solder paste printing, verified placement programs, measured reflow profiles, layered inspection, electrical testing, and closed-loop corrective action. Track defect rates by lot and process step so that drift is found early.