Phone: +86-137 5102 2384
Phone: +86-137 5102 2384
Oct. 13, 2026
Share:
Scaling PCBA from 10 to 10,000 units is not simply a larger purchase order. The transition from a PCB assembly prototype to mass production changes how you manage the BOM, DFM, SMT yield, testing, suppliers, and production documentation. Teams searching for low-volume to high-volume PCB assembly often face the same risks: parts become unavailable, a prototype design fails automated assembly, and a small defect rate becomes hundreds of failed boards. A controlled NPI process and one-stop PCB assembly partner such as Benewave can reduce these risks by turning design assumptions into measurable manufacturing requirements.
A 10-unit build can sometimes tolerate manual placement, substitute components, and engineering rework. A 10,000-unit build cannot rely on informal decisions. If one missing resistor delays a small prototype, the impact may be limited. If the same resistor is unavailable after production has been scheduled, the line may stop, the delivery date may move, and thousands of partially completed boards may require rework.
The cost structure also changes. At low volume, labor and setup costs may dominate. At high volume, component pricing, placement efficiency, first-pass yield, test coverage, warranty exposure, and inventory risk become more important. The right objective is not only to obtain a lower unit price. It is to achieve repeatable quality with controlled variation from the first production lot through the final shipment.
The first common problem is an incomplete or unstable bill of materials. A prototype BOM may contain manufacturer part numbers that are obsolete, approved alternatives that were never tested, or quantities that do not account for production scrap and feeder setup. It may also omit package information, moisture sensitivity level, lifecycle status, or approved substitute rules.
This becomes a major problem when moving from a PCB assembly prototype to mass production. A part that was available for 10 units may have a long lead time, a minimum order quantity of several thousand pieces, or an end-of-life notice. Using an unqualified substitute can change electrical performance, thermal behavior, mechanical fit, or regulatory compliance.
How to solve it:
For regulated or safety-related products, the BOM should also identify materials and components relevant to RoHS, REACH, conflict minerals, or sector-specific requirements. The European Commission explains that RoHS restricts specific hazardous substances in electrical and electronic equipment. See the European Commission RoHS overview for the current regulatory framework.
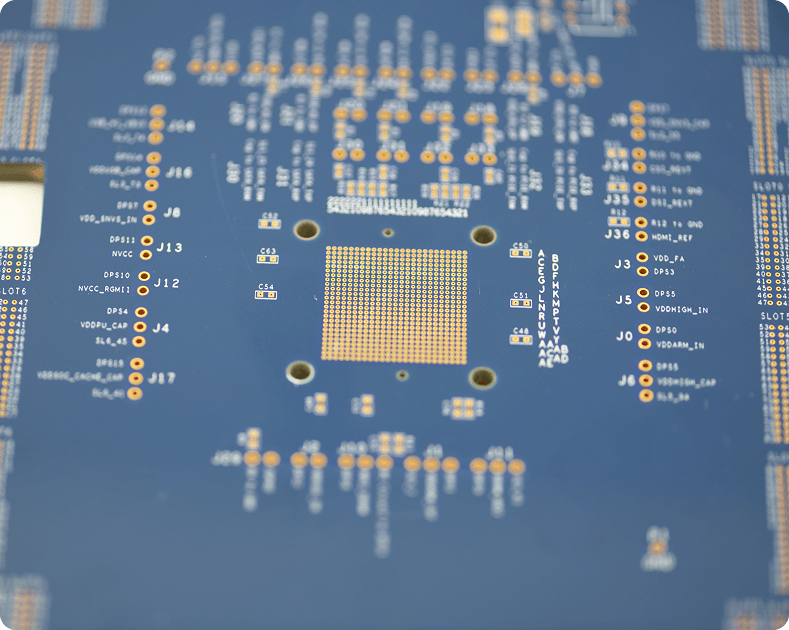
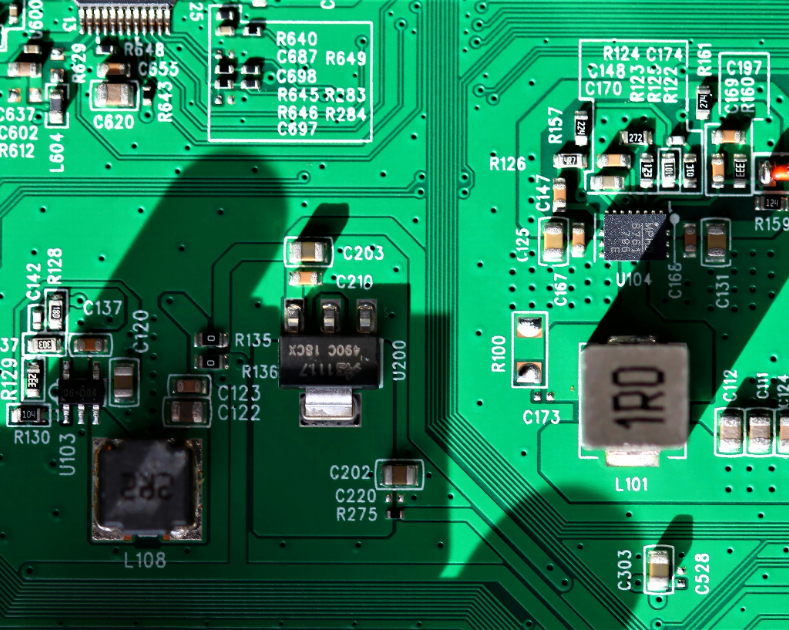
A board that works electrically may still be difficult or expensive to assemble. Common design-for-manufacturing and design-for-assembly problems include insufficient component-to-component clearance, limited access for inspection, inconsistent fiducial placement, unsuitable panelization, small solder mask openings, and components placed too close to the board edge.
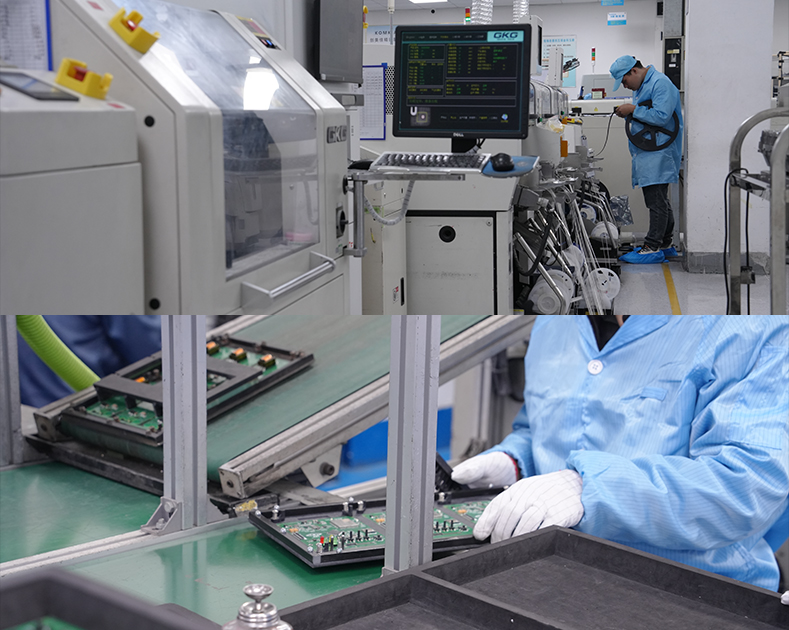
Prototype assembly can hide these issues because technicians may place parts manually or correct them during rework. At 10,000 units, the same design can produce recurring solder bridges, tombstoning, skewed components, insufficient solder, or an excessive number of manual operations.
How to solve it:
IPC publishes widely used standards for electronics manufacturing, including IPC-A-600 for printed board acceptability and IPC-A-610 for electronic assembly acceptability. These standards do not replace a product-specific drawing or customer specification, but they provide a common foundation for workmanship requirements. The official standards information is available through the IPC standards portal.
Yield is often the point at which a prototype process is exposed as unsuitable for volume. A line producing 98 percent first-pass yield may appear acceptable for 10 boards, but at 10,000 units it could imply approximately 200 boards requiring rework or investigation. The exact result depends on the defect definition and whether yield is measured per board, per placement, or per process step.
Typical causes include incorrect stencil thickness, poor solder paste storage, excessive paste age, inaccurate component libraries, feeder errors, inadequate thermal profiling, warped boards, and variations in component termination finish.
How to solve it:
Do not present a generic yield percentage as a guarantee. A responsible supplier should identify the measurement method, sample size, defect classification, and corrective action process. For workmanship acceptance, the applicable IPC class and customer requirements should be documented in the quality plan.
Scaling PCBA often exposes supply-chain risk before it exposes an assembly problem. A prototype may use distributor stock, while a production order requires factory allocation. Lead times can also vary by package, semiconductor category, geographic source, and market conditions.
One unavailable microcontroller can hold an entire finished-goods shipment even when every other component is in stock. Buying excessive material is not a complete solution because demand may change, components may become obsolete, and moisture-sensitive or date-sensitive materials may require controlled storage.
How to solve it:
The U.S. National Institute of Standards and Technology supply chain risk management guidance emphasizes identifying, assessing, and managing supply-chain risks. Its principles are applicable to electronics procurement even when the product is not a government system.
A prototype may be checked by powering it on and confirming several functions. That level of testing is rarely sufficient for 10,000 units. A board can pass visual inspection while containing an open circuit, an intermittent solder joint, a wrong-value component, a programming error, or a marginal power rail.
Testing should be designed together with the product and PCB, not added after the board has been routed. The choice between flying probe, in-circuit test, functional test, boundary scan, programming verification, and end-of-line system test depends on volume, access, coverage, fixture cost, test time, and product risk.
How to solve it:
For higher-volume production, test time directly affects capacity. For example, reducing an end-of-line test from 60 seconds to 30 seconds can double the theoretical station throughput if all other constraints remain unchanged. Actual capacity will still depend on fixture loading, operator handling, retest policy, downtime, and bottleneck balance.
Many production failures are configuration failures rather than soldering failures. The contract manufacturer may receive a new Gerber package but an old BOM, an updated firmware file without a revision change, or assembly drawings that do not match the panel version. When 10,000 units are involved, an uncontrolled change can affect an entire lot.
How to solve it:
Document control is especially important when several vendors are involved. A one-stop PCB assembly supplier can reduce transfer errors by coordinating sourcing, fabrication, SMT, testing, and delivery, but the customer still needs to approve the configuration baseline.
Moving directly from 10 units to 10,000 units creates unnecessary risk. The first production run should prove more than whether the board powers on. It should validate material substitutions, panelization, feeder setup, stencil performance, soldering profile, test fixtures, operator instructions, packaging, and traceability.
Capacity should also be calculated from cycle time and available production hours rather than from a supplier statement that a line is "high capacity." If one board takes 45 seconds of constrained assembly time, the theoretical output is 80 boards per hour at that operation. Actual output will be lower after changeovers, downtime, inspection, replenishment, rework, and scheduled breaks.
How to solve it:
A pilot lot does not need to be the same size for every product. A simple two-layer controller with stable components may need less process validation than a dense multilayer board with fine-pitch BGA packages, high-speed interfaces, or strict impedance control.
Why: A controlled data package prevents the assembler from manufacturing from mismatched revisions.
Operation method: Create a release checklist covering the schematic, PCB layout, fabrication files, assembly files, BOM, approved vendor list, drawings, firmware, test procedure, packaging specification, and regulatory requirements. Perform a revision cross-check before quotation and again before material purchasing.
Best for: Every project, especially products developed by separate electrical, mechanical, firmware, and procurement teams.
Why: Design changes are less expensive before stencil, fixture, and bulk material commitments.
Operation method: Ask the manufacturing partner to review pad geometry, component spacing, panel rails, fiducials, test access, thermal zones, connector handling, and depanelization. Record each finding with a decision, owner, and revision reference.
Best for: Fine-pitch SMT, BGA, high-density boards, rigid-flex assemblies, and products moving from hand assembly to automated placement.
Why: A qualified alternate can prevent a single component from stopping a complete production order.
Operation method: Classify parts as standard, preferred, critical, single-source, lifecycle-sensitive, or customer-specified. Approve alternates through electrical comparison, sample testing, and documented engineering approval. Do not substitute a component only because its value and package appear identical.
Best for: Products using semiconductors, connectors, sensors, wireless modules, displays, or parts with long procurement cycles.
Why: Measured data shows whether the process is stable instead of relying on visual confidence.
Operation method: Track solder paste inspection results, AOI defects, first-pass yield, rework, scrap, functional test failures, and defect Pareto categories during the pilot. Define acceptance limits before reviewing the results. Investigate repeated defects with a documented corrective action such as 8D or a root-cause analysis.
Best for: Products with safety implications, warranty exposure, high rework cost, or a large gap between prototype and planned production volume.
Why: Detecting a defect at the production station costs less than discovering it after shipment or field installation.
Operation method: Add test points, programming access, serial number marking, fixture interfaces, and software test hooks during the design stage. Define whether each board receives visual inspection, AOI, electrical test, functional test, programming verification, or a combination of these methods.
Best for: Connected products, power electronics, industrial controls, medical devices, automotive electronics, and products where field replacement is expensive.
When comparing suppliers, ask for more than a unit quotation. Request the proposed NPI workflow, DFM review format, component sourcing policy, quality standards, inspection points, test capability, traceability method, change-control process, and production capacity calculation.
Benewave can be evaluated as a one-stop PCB assembly option when the project requires coordinated PCB fabrication, component sourcing, SMT assembly, through-hole processing, inspection, programming, functional testing, and shipment. The customer should still confirm the exact capabilities and acceptance criteria for each project, including board dimensions, layer count, package types, minimum pitch, BGA requirements, surface finish, impedance control, testing, and applicable compliance documentation.
The seven main risks are unstable BOM data, poor DFM and DFA, low SMT yield, component shortages, late testing, weak revision control, and an unrealistic ramp schedule. The practical solution is a staged NPI process that starts with production-ready documentation and continues through design review, material qualification, pilot assembly, measured process validation, controlled ramp-up, and traceable final testing.
For a 10-unit prototype, manual correction may hide process weaknesses. For 10,000 units, those weaknesses become measurable cost, schedule, and reliability problems. A disciplined low-volume to high-volume PCB assembly strategy uses qualified components, documented acceptance criteria, AOI, functional testing, impedance control where required, and professional change management to make the scale-up repeatable.
There is no universal number. The appropriate pilot size depends on board complexity, component risk, test coverage, regulatory requirements, and the maturity of the design. A pilot should be large enough to expose setup, material, soldering, testing, and packaging issues. The decision to move forward should be based on documented exit criteria rather than unit count alone.
The most important requirement is a synchronized release package, not one individual file. The BOM, PCB fabrication data, pick-and-place data, assembly drawing, firmware, test procedure, and revision history must describe the same product configuration.
You can use them if they meet production availability, lifecycle, package, performance, compliance, and qualification requirements. Prototype availability does not prove that a component is suitable for 10,000-unit production. Check manufacturer status, authorized sourcing, lead time, minimum order quantity, and approved alternates.
No. AOI can identify many visible assembly defects, but it cannot replace every electrical or functional test. Hidden solder joints, wrong firmware, marginal power behavior, intermittent connections, and system-level faults may require flying probe, in-circuit test, boundary scan, programming verification, or functional testing.
Ask how the supplier handles DFM feedback, component substitutions, incoming inspection, moisture-sensitive devices, stencil design, reflow profiling, AOI, X-ray inspection when applicable, functional testing, traceability, nonconforming material, engineering changes, capacity planning, and warranty returns. Also request measurable definitions for yield, rework, delivery performance, and acceptance criteria.
Impedance control should be reviewed during schematic and PCB layout planning, before fabrication data is released. The required stackup, dielectric material, trace width, spacing, copper thickness, and manufacturer tolerance should be agreed with the fabricator. It should not be treated as a last-minute fabrication note for high-speed or controlled-impedance interfaces.
Successful scaling PCBA depends on the same fundamentals at every volume: controlled BOM data, manufacturable layout, qualified materials, stable SMT yield, measurable testing, traceability, and disciplined production change control. These professional terms are not paperwork additions; they are the operating system for reliable PCB assembly prototype to mass production.
Find Partners, Not Just Suppliers
Expert OEM & PCBA manufacturing tailored to your exact specifications. Contact us today to discuss your project and discover a more collaborative way to manufacture.
Get a Fast Quote & Free DFM Review
Related PCB Assembly Service